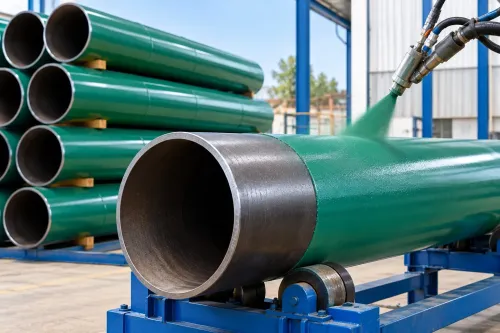
A single protective layer may meet the requirements of many pipeline projects, while other applications call for additional performance characteristics. Dual FBE Coating uses two fusion bonded epoxy layers designed to work as a combined system, and it may be specified where project conditions require properties beyond those expected from a standard single-layer configuration.
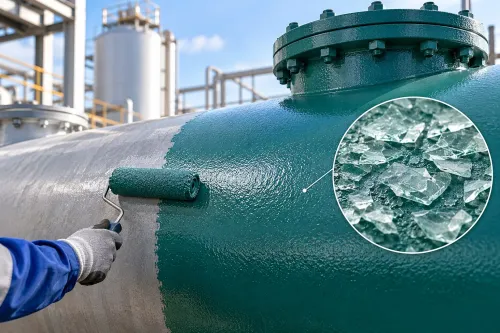
The first layer typically performs the primary corrosion-protection role by bonding to the prepared steel substrate. A second compatible FBE layer is then applied to provide additional characteristics defined by the coating system and project specification.
The reason for specifying a dual system should always be clear. Adding another layer should not be treated as an automatic upgrade for every pipeline.
Project engineers may evaluate dual-layer FBE where pipeline construction, handling, installation or service conditions create particular protective requirements. The actual suitability and performance characteristics depend on the selected coating products and specified system.
Several questions help determine whether a dual system deserves consideration:
- What environmental conditions will the pipeline encounter?
- How will coated pipe be handled and installed?
- Is additional mechanical protection required by the specification?
- What operating temperatures are expected?
- Which coating standard or client specification applies?
- How will the completed coating be inspected?
Application control is particularly important because both layers must form the intended system. Surface preparation before the first coat, temperature management, timing between layers, total coating thickness and curing need to follow the approved procedure.
For pipeline and infrastructure businesses in Ahmedabad and across Gujarat, logistics should be included in this assessment. Long pipes and heavy components may pass through several handling stages between fabrication, coating, transport and installation. The specified coating system should be considered alongside those real project conditions.
Heatman Products Pvt Ltd can review industrial coating enquiries from Ahmedabad when buyers provide pipe dimensions, quantities, technical specifications and intended service conditions. This information is more useful than requesting “dual FBE” without explaining the application.
Inspection requirements should also be agreed before production. Depending on the specification, checks may include coating appearance, thickness and holiday detection, together with other specified quality-control procedures.
Commercial comparison needs similar discipline. Buyers should verify that competing quotations refer to equivalent coating systems, thickness requirements, preparation standards and inspection scope.
Dual FBE coating makes sense when the second layer addresses a defined technical requirement within an engineered coating system. It should not be selected simply because two layers sound more protective than one.
When the pipeline environment, construction method and project specification are clearly defined, engineering teams can determine whether a dual-layer system is justified and establish the quality controls needed during application.
Keywords